
Bundling
Members are bundled by type and length, with bundle weights and lifting points recorded so the container plan and site crane capacity match the load.
Project Case
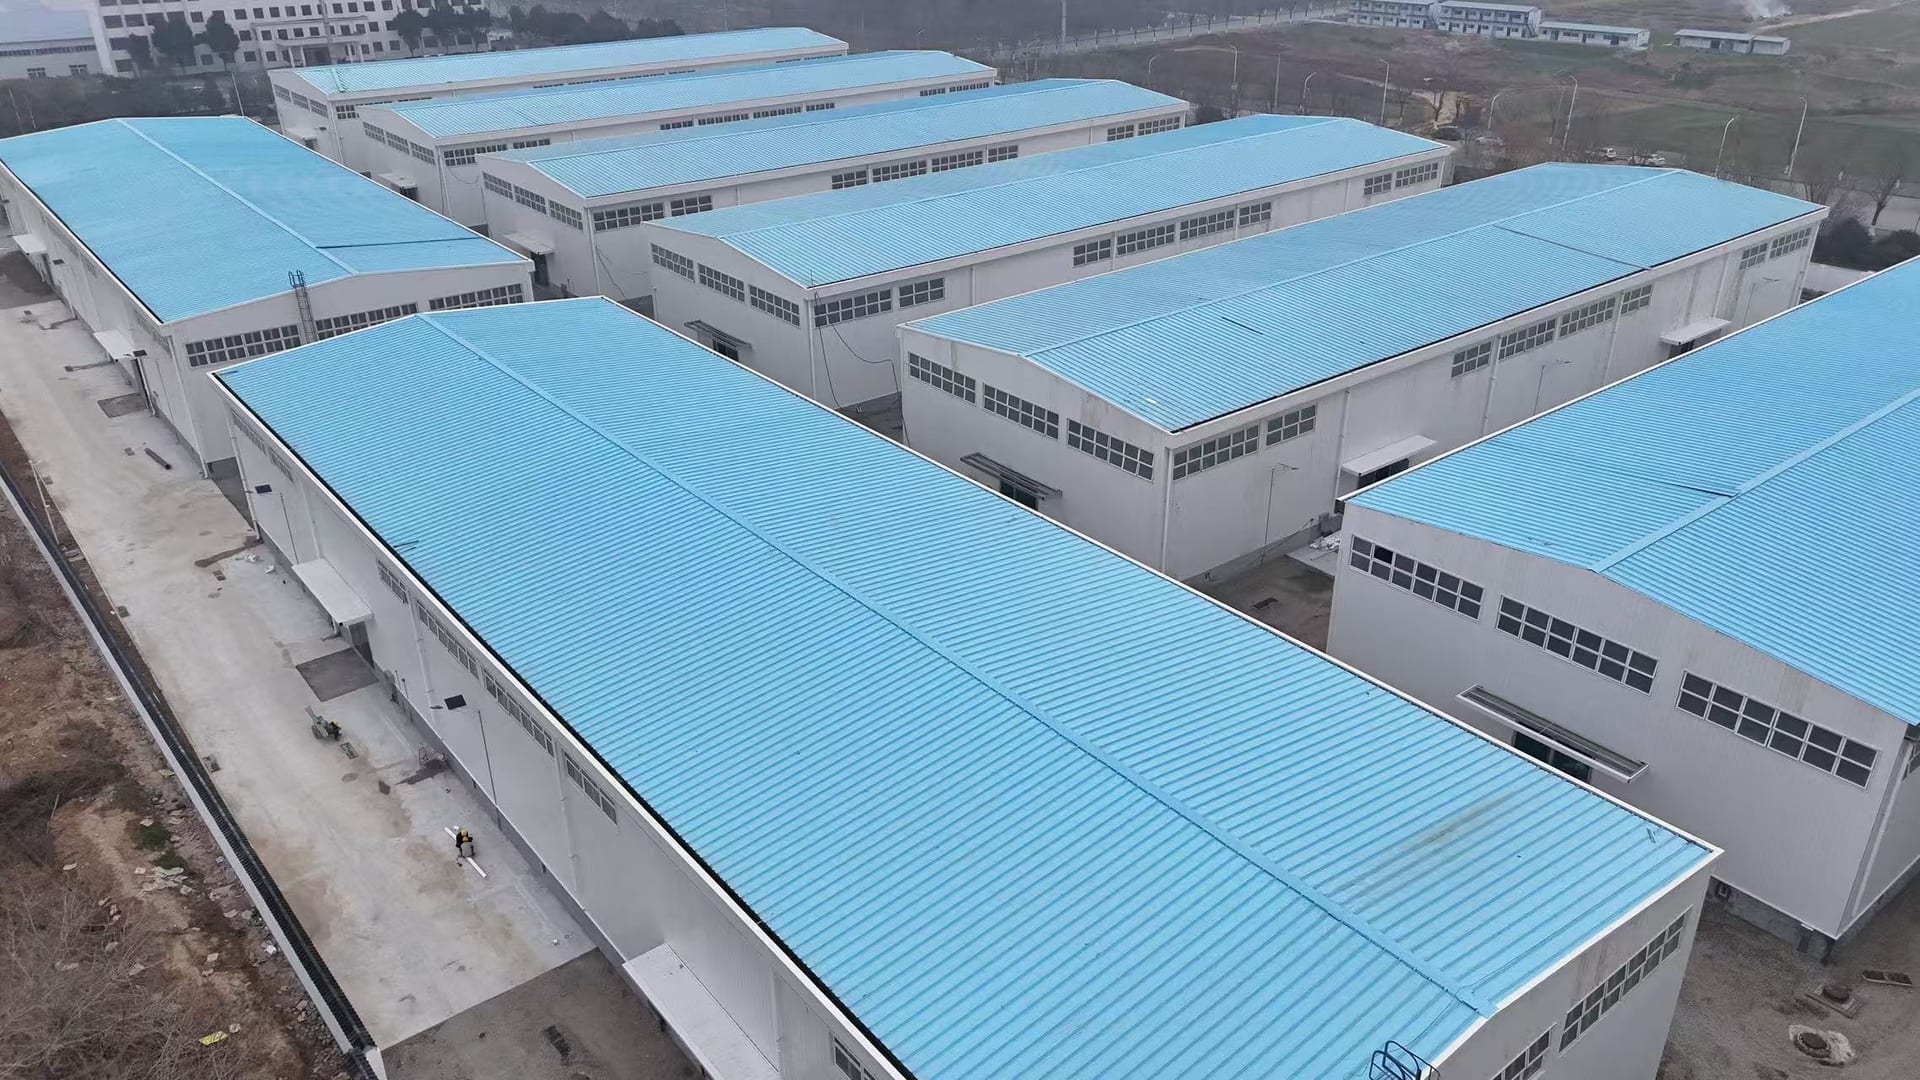
Steel structure works for five warehouse buildings in a logistics and distribution park, fabricated and delivered as one package.
Confirmed case facts
These figures were provided by the company for this project. The client name is not published.
Fabrication scope
The photograph illustrates this building type. It is not a photograph of this project.
Standard route
The sequence below is the standard fabrication route. The specific inspection scope and standards are confirmed for each project.
Material identity, dimensions and documentation are checked against confirmed project requirements.
Approved member information guides plate and section preparation.
Components are fitted and checked against approved fabrication information.
Welding requirements and inspection scope follow confirmed project documentation.
Member geometry is checked and corrected within the confirmed acceptance criteria.
Surface preparation requirements must be confirmed before processing.
Coating system, color, dry-film requirements and repair method require project confirmation.
Marks, bundles, protection and loading sequence are reviewed before shipment release.
Quality control
These are the control points applied before a member or bundle is released.
Steel grade, heat number and mill test certificates are checked against the approved material list before any plate or section is cut.
Component length, hole diameter, hole group position and edge preparation are measured against the approved shop drawings.
Fit-up, root gap, camber and weld leg size are checked before welding. Weld procedures and welder qualification follow the standard specified for the project.
Overall length, squareness, member straightness, connection locations and hole groups are measured after welding and before surface treatment.
Shot-blast grade, coating dry film thickness or galvanizing coverage are inspected and recorded against the coating specification.
Bundle contents, piece marks, protection of connection faces and the loose-part list are checked against the packing list before loading.
Packing and delivery
Packing, marking and loading preparation follow the same sequence for every order.
Members are bundled by type and length, with bundle weights and lifting points recorded so the container plan and site crane capacity match the load.
Every bundle carries a piece mark, bundle number and project reference that match the packing list and the erection drawings.
Connection faces, machined surfaces, coated edges and insulated panels are protected for sea freight. Loose parts are packed and itemised separately.
Loading plans use 40HQ, 40OT or 20GP containers, with the sequence set by component weight, length and the unloading order at site.
Related cases
Luohe, Henan Province, China
Eight cotton storage warehouses, covering steel structure fabrication and installation, with a combined floor area of 15,448 m2.
Fugou County, Zhoukou, Henan Province, China
Steel structure works for three factory workshop buildings at a building materials production site, with a combined floor area of 12,876 m2.